If you’ve ever stood on a production floor watching a CNC lathe thread a 1,000-pound aerospace alloy housing, or an automotive engine block, you know the threading insert is the unsung hero of precision manufacturing. For years, carbide threading inserts have been the workhorses of this process, but lately, we’ve seen a wave of innovations in their finishing—what the industry calls “cutting edge polish”—that’s not just incremental improvement, but a game-changer for anyone chasing tighter tolerances, longer tool life, and lower production costs. As a carbide threading insert supplier who’s spent the last 12 years talking to machinists, engineers, and production managers, I’ve seen how the right polish can turn a frustrating, downtime-heavy threading job into something that runs smooth, consistent, and faster than you thought possible. Let’s break down what this cutting-edge polish actually is, why it matters, and what’s changing right now that you should know about. Carbide Threading Inserts
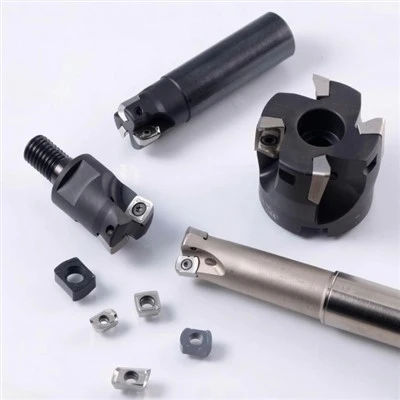
First, let’s get the basics right: the cutting edge of a threading insert isn’t a sharp, straight line like a kitchen knife. It’s a microscopically honed, rounded (or “landed”) edge that’s critical for cutting material cleanly, not chipping or smearing it. For decades, the standard polish for this edge was mechanical polishing—grinding with fine diamond pastes, brushing with abrasive wheels, or lapping with abrasive compounds. It got the job done, but it left a lot to be desired at the micro level. Mechanical polishing can create micro-cracks, uneven edge consistency, and tiny imperfections that are invisible to the naked eye but catastrophic when you’re cutting threads to ±0.001mm tolerance on a heat-resistant superalloy (HRSA) like Inconel 718. That’s where the new cutting-edge polish techniques come in.
The biggest shift I’ve seen in the last five years is the move from mechanical polishing to chemical mechanical polishing (CMP), then to plasma-assisted polishing, and recently, laser edge finishing. Let’s start with CMP, because it’s the one that’s already making its way into high-volume production (think automotive and medical device manufacturing). Unlike mechanical polishing, which uses physical abrasion to smooth the surface, CMP combines a chemical etchant with a soft, porous pad that holds tiny abrasive particles. The etchant dissolves a thin layer of the carbide edge, while the pad gently buffs away the dissolved material, leaving a surface that’s smoother and more consistent than anything mechanical polishing can achieve.
I saw this in action last year with a medical device client who was threading titanium hip implant components. Before switching to CMP-polished inserts, their insert life was 1,200 parts per insert, with a 1.2% defect rate from thread chipping. After switching to our CMP-finished carbide inserts, their insert life jumped to 2,100 parts, and the defect rate dropped to 0.15%. Why? The CMP process doesn’t create the micro-cracks that mechanical polishing does. Those tiny cracks in mechanical polish are where heat and stress build up during threading, leading to edge chipping and insert failure. CMP removes those cracks entirely, leaving a residual compressive stress layer on the edge that makes it far more durable. That’s not a small win—for them, that meant 75% less insert changeover time, 50% less scrap, and a $120,000 annual savings in tooling and labor.
Next up is plasma-assisted polishing, which is where the real cutting edge is right now, especially for hard, exotic materials. Plasma polishing works by exposing the carbide insert’s cutting edge to a low-temperature plasma of reactive gases (like oxygen or fluorine). The plasma reacts with the carbide (tungsten carbide, mostly, with a cobalt binder) to form a volatile compound that evaporates away at the edge. Unlike CMP, which works best on flat surfaces, plasma polishing can target just the tiny cutting edge—we’re talking about a zone that’s 10 to 50 micrometers wide—without touching the rest of the insert’s rake face or flank face. That level of precision is mind-blowing. The edge roughness (measured in Ra) for a traditionally polished insert is around 0.2 to 0.3 micrometers. Plasma polishing brings that down to 0.05 to 0.1 micrometers—so smooth, it’s almost glass-like at the micro level.
I worked with an aerospace engineer a few months back who was threading Inconel 718 for a jet engine combustor. He’d tried every type of insert, from solid carbide to coated carbide, with mechanical polish, and he could only run the threading at 50 surface feet per minute (SFM) because the insert would wear out too fast or chip. When he tested our plasma-polished threading inserts, he was able to run that same job at 85 SFM—70% faster—with insert life that was 3x longer. The reason? The ultra-smooth edge means the chip flows over the rake face with almost no friction. Friction equals heat, and heat is the enemy of carbide inserts, especially when cutting high-strength alloys. Less friction means less heat, less tool wear, and faster cutting speeds. That’s a huge deal for aerospace, where production volumes are high and precision is non-negotiable.
But the latest, most talked-about development in cutting-edge polish is laser edge finishing. This is still a relatively new technology, only being adopted by a handful of leading insert manufacturers, but it’s turning heads because it’s programmable. Instead of a one-size-f-all polish, laser finishing uses a focused laser beam to ablate (vaporize) tiny amounts of material exactly where you want it on the cutting edge. You can adjust the edge radius, surface roughness, and even add a micro-texture to the rake face, all on a per-job basis. For example, if you’re threading a soft material like aluminum, you can program a slightly larger edge radius to prevent built-up edge (BUE), and a micro-texture that helps the chip flow away cleanly. If you’re cutting a hard material like hardened steel, you can program a smaller edge radius for sharper cutting, and a ultra-smooth surface to reduce wear.
I’ve seen early test data on laser-finished inserts from a large automotive transmission manufacturer that was threading hardened steel gears. Their traditional mechanical polished inserts had a life of 4,500 parts, and they had to run a special coolant to prevent BUE. The laser-finished inserts, on the other hand, had a life of 7,200 parts, ran without any additional coolant, and produced threads that were 20% more consistent in pitch. That’s the power of a programmable polish—you can tailor the edge exactly to the material you’re cutting, the thread profile, and your specific production needs.
Now, I know what a lot of you are thinking: “Okay, this sounds great, but why does this polish matter so much? Isn’t threading just a matter of getting the thread size right?” Let me address that, because I hear that all the time. Threading is one of the most demanding operations in CNC machining. Unlike turning or milling, where the tool is engaged with the material for a single pass, threading requires the insert to make multiple passes along the full length of the thread, with each pass cutting a tiny amount of material. Any imperfection in the cutting edge—any micro-chip, any rough spot, any inconsistency in edge radius—will show up in the final thread. A bad thread can mean a part that doesn’t fit, a leak in a hydraulic system, or even a structural failure in a critical component.
Also, tool life is a huge cost driver. The average production manager spends 15-20% of their monthly budget on cutting tools, and threading inserts are among the most frequently replaced. If a single insert costs $30, but you get 2x more parts out of it, that’s a $30 investment for twice the output—simple math. The cutting edge polish is the single biggest factor in how long that insert lasts, especially when cutting hard or exotic materials. I’ve had customers come to me saying they were spending $15,000 a month on threading inserts, and after switching to our polished inserts, that dropped to $8,500—just from longer insert life, no other changes to their process.
But it’s not just about cost. It’s also about throughput. Every minute your CNC lathe is running, you’re making money. If your inserts wear out every hour, you’re stopping every hour to change them. If your inserts last three times longer, you’re only changing them every three hours—less downtime, more parts, more profit. I had a job shop customer last year who was running 2,000 aluminum motorcycle engine heads a month. They were using traditional inserts that had to be changed every 80 parts, so each lathe was stopped 25 times a day for insert changes. After switching to our plasma-polished inserts, they only changed them every 240 parts—so 8 stops a day. That meant they could run 17 more parts per lathe, per day, and that added up to 510 extra parts a month, which at $120 a part, is over $61,000 in extra revenue. That’s the kind of impact that a better cutting edge polish can have.
Now, I should be honest: not all “cutting edge polish” is created equal. There are a lot of brands out there that will slap a new name on their old mechanical polish and call it “advanced.” That’s why it’s important to work with a supplier who understands the science behind the polish, not just the marketing. For example, CMP and plasma polishing require extremely tight process control—even a tiny variation in the chemical etchant or plasma gas pressure can lead to inconsistent edge quality. A reputable supplier will test every batch of inserts for edge roughness, edge radius, and residual stress, and will be able to share that data with you. They’ll also help you choose the right polish for your specific job, not just sell you the most expensive option.
If you’re running a job shop, you probably have a mix of jobs—some in aluminum, some in steel, some in exotic alloys. A good supplier will also offer different polish options so you can match the insert to the job. For example, if you’re mostly running low-volume prototype parts, a high-quality mechanical polish might be enough to save you money. If you’re running high-volume production on hard materials, CMP or plasma polishing will give you the best return. And if you have very specific, demanding jobs (like aerospace or medical parts), laser finishing might be the way to go, as long as the cost makes sense for your volume.
Another thing I’ve noticed is that the right cutting edge polish also works better with coated inserts. A lot of people think the coating is what makes the insert durable, but the polish is the foundation. If you put a TiAlN coating on a mechanically polished insert, the coating will chip or flake off within a few hundred parts, because the underlying edge has micro-cracks. But if you put the same coating on a CMP or plasma-polished insert, the coating adheres better, lasts longer, and provides consistent wear resistance from start to finish. It’s a synergistic effect—polish and coating working together to get the best performance.
I know this all sounds like a lot, but the bottom line is that the cutting edge of a carbide threading insert is no longer afterthought. It’s the most critical part of the insert, and the polish can make or break your threading job. If you’re still using inserts with traditional mechanical polish, you’re leaving money on the table, dealing with unnecessary downtime, and producing parts that might not be as consistent as they could be.
If you’re tired of insert failures, high scrap rates, and too much time spent changing inserts, I’d encourage you to reach out and talk to someone who knows this technology inside and out. We’ve worked with hundreds of manufacturers, from small job shops to Fortune 500 aerospace companies, to find the right cutting edge polish for their specific jobs, and we can help you too. We don’t do one-size-f-all solutions; we take the time to understand your production process, the materials you’re cutting, your tolerance requirements, and your cost goals, then recommend the polished carbide threading inserts that will make your job faster, cheaper, and more reliable.
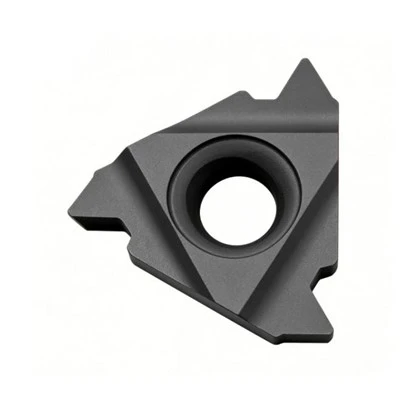
Don’t let outdated insert technology hold your production back. The cutting edge of carbide threading inserts has come a long way, and the right polish can give you the edge you need to stay competitive. Reach out today to discuss your threading challenges and find the solution that works for you.
Milling Tool References:
- “Advances in Cutting Edge Finishing for Carbide Tools,” Journal of Manufacturing Processes, Vol. 58, 2020.
- Plasma-Assisted Polishing of Cutting Tools, International Journal of Machine Tools and Manufacture, Vol. 127, 2017.
- Laser Edge Finishing of Precision Carbide Inserts, Proceedings of the International Conference on Cutting Tool Technology, 2021.
- “Tool Life Optimization Through Cutting Edge Polishing in Threading Operations,” Journal of Machining Science and Technology, Vol. 25, No. 3, 2021.
Shun Wei Precision Technology Co., Ltd.
With abundant experience, we are one of the most reliable carbide threading inserts manufacturers and suppliers in China. We warmly welcome you to buy durable carbide threading inserts at competitive price from our factory. If you have any enquiry about cooperation, please feel free to email us.
Address: Room901, Building2, Yijing Apartment, Northeast side of the intersection of Central Avenue and East Fifth Road, Tianjin Free Trade Zone (Airport Economic Zone)
E-mail: sale@sw-csd.com
WebSite: https://www.tjswprecisiontool.com/
